SAT vs. FAT in Diagnostic Manufacturing, and What Each Test Covers
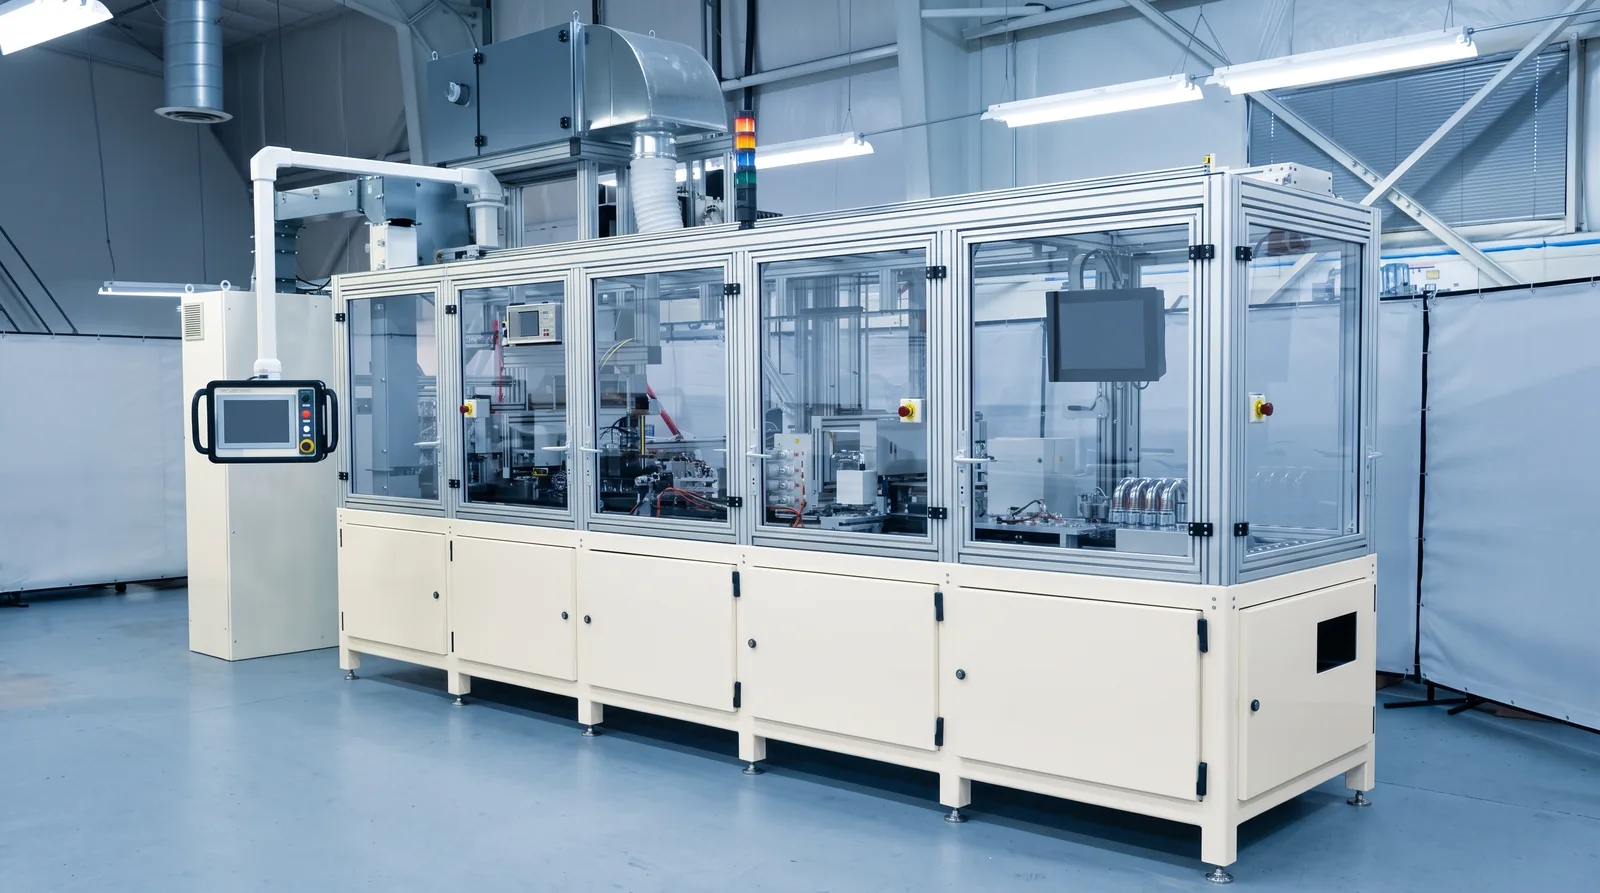
SAT vs FAT comes down to location and risk. FAT proves the machine works at the vendor against the URS before shipment. SAT proves it still works at your site, with your utilities and systems, before qualification.
- FAT happens at the vendor, before shipment.
- SAT happens at your site, after installation and before IQ.
- FAT catches what the vendor controls.
- SAT catches transit damage, utilities, environment, and integration.
- The punch list from FAT becomes the scope of SAT, and good traceability to the URS keeps IQ and OQ short.
A machine that passes FAT can still fail at your site. Transit knocks a camera loose. Your humidity differs from the vendor’s. The MES handshake behaves differently on your network.
That’s why you need both tests. As a fractional automation engineer, I run FAT and SAT on diagnostics equipment, and the confusion between them costs buyers time and money.
This post covers where each test sits, what each one catches, and how the handoff works. It sits beside the FAT checklist.
FAT vs. SAT at a glance
| Dimension | FAT | SAT |
|---|---|---|
| Location | Vendor’s site | Your site |
| Timing | Before shipment | After installation, before IQ |
| Main question | Did the vendor build what the URS asked for | Did it survive shipping and does it work here |
| Catches | Design errors, build defects, software bugs | Transit damage, utilities, environment, integration |
| Cost to fix | Low, the vendor’s team is on hand | Higher, the machine is on your floor |
| Output | Executed protocol, punch list | SAT report, closed punch list |
Kneat gives the same split on location and timing, with FAT before shipment and SAT after installation and before IQ.
Where each test sits in the sequence
The usual lifecycle runs URS, DQ, vendor selection, FAT, shipping and installation, SAT, IQ, OQ, and PQ. FAT and SAT build evidence for qualification. They don’t replace it.
Sequence isn’t rigid. The GMP Compliance Adviser says SAT is typically done before IQ, and that the order depends on project framework and equipment type. Your quality procedure decides. Some sites fold SAT activities into IQ. Write it into the validation plan.
Lab Manager notes that a well-executed FAT can shrink IQ scope at site, and that SAT follows installation and comes before formal IQ. That matches my experience. In my projects, IQ and OQ belong to engineering. PQ belongs to quality, who build product and confirm the full process.
What FAT can’t tell you
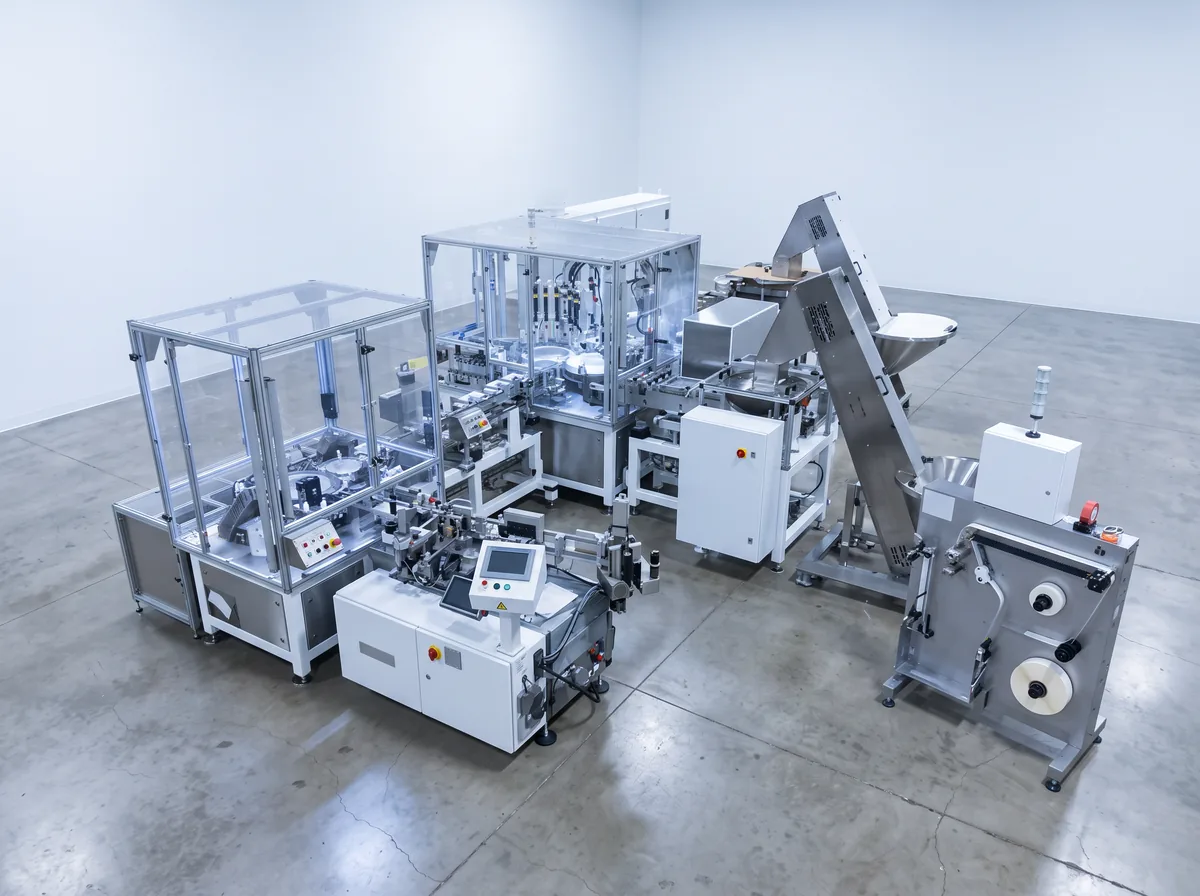
Vendors can’t always test at full conditions. Paul Mueller points out that the manufacturer’s plant may not be equipped to test at full capacity or with every product component. A SAT shows how it runs under your real conditions.
SAT also covers transport. PQE Group says SAT provides documented evidence that the equipment arrived in good condition and wasn’t affected by transportation.
Some items just can’t happen at the vendor. A food-industry equipment engineer told PackWorld that tests like vacuum and gas monitoring get converted to SAT. Diagnostics lines have the same category. Your humidity, your compressed air, your network.
How the punch list turns into the SAT scope
Everything found at FAT becomes the SAT scope. The machine ships. SAT repeats the FAT with every punch item verified, and checks that nothing broke in transit. That’s the whole loop.
Run one punch list across both tests. If it splits into two documents, items go missing between them.

Don’t repeat work you’ve already proven
Re-running every test at IQ and OQ wastes weeks. A Manufacturing Chemist article reports that nearly half of companies repeat FAT and SAT tests during IQ and OQ, often because Quality wasn’t involved early.
ISPE’s GAMP 5 Second Edition, published in July 2022, stresses leveraging suppliers and their documentation. Bring Quality into the FAT protocol review so they’ll accept the evidence later.
If the FAT and SAT trace to the URS, the FAT document splits cleanly into IQ and OQ. Miss requirements and you invent new tests right when management wants product. By validation, you should already know everything about the machine. Validation just documents it.
The regulatory layer, briefly
The FDA’s QMSR, effective February 2, 2026, incorporates ISO 13485:2016 into 21 CFR Part 820. Your validation plan should say how FAT and SAT evidence feeds process validation. That’s a document decision, not a test.
Best for buyers planning acceptance for a new line.
- Scenario one. You’re writing the validation plan. Decide whether SAT stands alone or folds into IQ.
- Scenario two. Quality wants to repeat every test. Show them the FAT evidence and the traceability matrix.
- Scenario three. The vendor wants to skip SAT. Don’t. Transit and site conditions are yours.
Next step
Decide who owns each test, what the pass criteria are, and where the punch list lives. Do it before the PO is signed. See the URS guide for how to write requirements that tests can prove.
A 30-minute Manufacturing Automation Assessment can map this plan to your project.
Questions about FAT and SAT
What’s the main difference between FAT and SAT?
Location and risk. FAT proves the build at the vendor. SAT proves the machine at your site.
Can I skip SAT if FAT passed?
No. FAT can’t test your utilities, your environment, or transit damage.
Does SAT come before or after IQ?
Usually before, though the order depends on your project and quality procedure.
Who runs SAT?
Your engineering team, with the vendor present to fix issues.
Can FAT evidence reduce IQ and OQ work?
Yes, if it traces to the URS and Quality accepts it early.
The Bottom Line
Decide who owns each test, what the pass criteria are and where the punch list lives before the PO is signed.
Reza Bashar at MEPSCo GAMP provides fractional automation engineering for medical diagnostic manufacturers, from URS development through FAT, SAT and IQ/OQ/PQ. If you are planning acceptance testing for a new line, we start with your URS.