Consumable Diagnostics Automation Starts With a Better URS
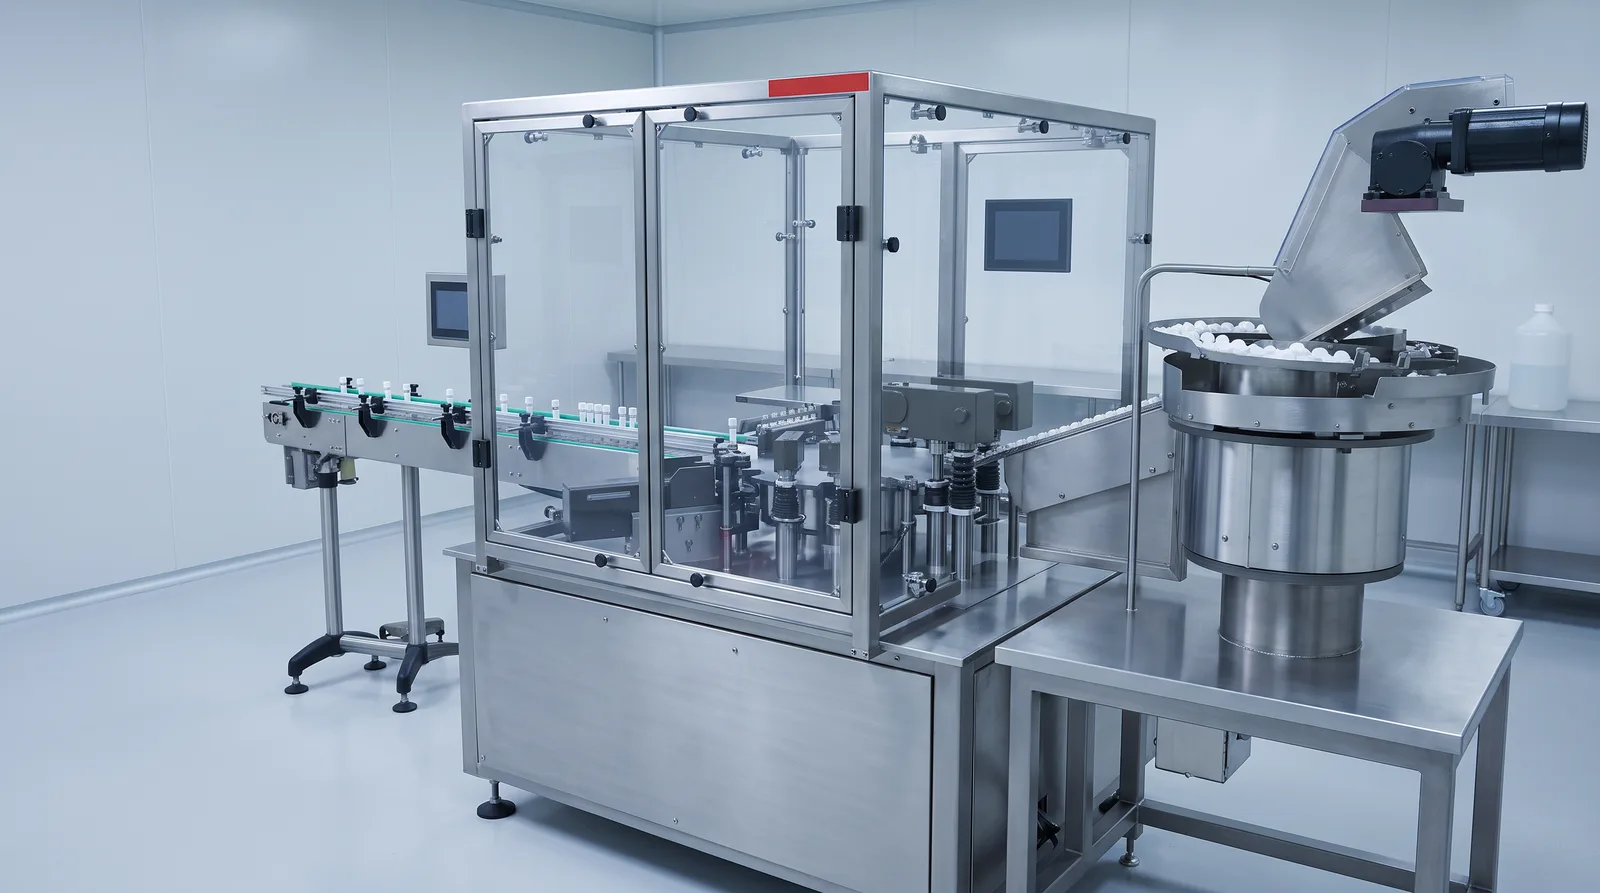
Consumable diagnostics automation is the custom equipment that fills, assembles, inspects, and packs test kits, cartridges, and lab components. It needs a URS built around the reagent, a vendor chosen on process proof, and a witnessed FAT.
- Consumable diagnostics lines go wrong at the purchase order, not on the floor, so the URS has to be written around the reagent and the consumable.
- Score vendors on process proof, such as documentation support, maintainability and experience with your reagent type, not on the lowest bid.
- Put a witnessed factory acceptance test in the contract, with an approved protocol, measurable pass criteria and punch-list rules.
- Choose to build, buy or use a contract manufacturer by how proven your demand is, and bridge with semi-automation while formats are still changing.
I procure automation for diagnostics manufacturers. As a fractional automation engineer, I sit on the buyer’s side of the table, and the same pattern shows up on troublesome projects. The machine is rarely the problem. The paperwork before the machine is.
A test kit line looks simple from the hallway. Fill a tube, cap it, label it, box it. Then the reagent foams. The cartridge needs a dry room. A format change eats a full shift. Every surprise becomes a change order, and every change order resets the schedule.
I hate change orders. So this post covers the three decisions that prevent the worst of them. How to write the URS, how to score vendors, and what the FAT has to prove. It also covers when to build, when to buy, and when to hand your first volume to a contract manufacturer. It’s written for makers of consumable diagnostics, lab-use components, and IVDs.
What makes a diagnostics line harder than a packaging line
Diagnostics consumable lines may combine small fill volumes, sensitive reagents, and tight humidity limits on one line. Cartridge work adds a second layer, because one weak weld can ruin a part that carries several reagents. Packaging-grade equipment wasn’t built for that mix, and the gaps show up at validation. Plan for them in the specification, not at the first run.
A cartridge scale-up guide from Invetech names ultrasonic welding, reagent deposition, drying, and sealing as the processes that carry the quality risk, and notes that a cartridge may deposit five reagents while only one is volume sensitive. One imperfect weld can still sink the part.
Humidity is the quiet one. Flex points out that cassette assembly belongs in a controlled low-humidity environment, with moisture barriers and desiccants protecting the reagents. One automation builder says its rapid-test line runs in a dry environment with no clean room required. Whether that fits your product depends on your risk analysis. LSO notes that ISO 13485 requires contamination control wherever the work environment can hurt product quality, and the test panel is yours to design from your own risk analysis.
Complexity climbs with the product too. A Swiss automation maker told Clinical Trials Arena that strip devices need only a few assembly processes, while molecular devices need many, because of the reagents and materials involved.
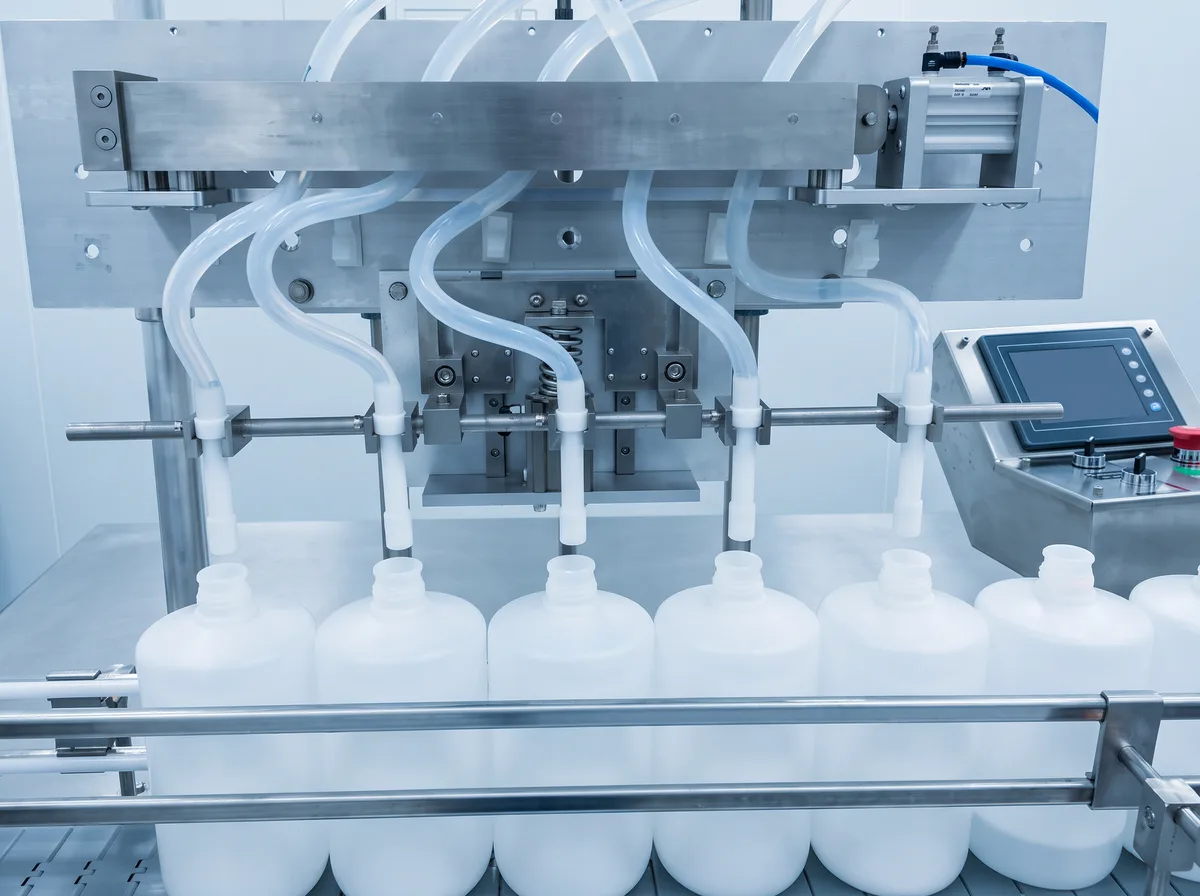
Then there are reagents that refuse to behave. On one small project, a custom nozzle and process filled just over a liter of foamy reagent inside the required 60 minutes. It beat the lab setup the customer started with. A stock filler wasn’t going to get there.
Write the URS around the reagent, not the machine
A URS states what the system must do, in testable terms, from the user’s side. A GAMP 5 overview describes it as clear, testable language that stays out of the design. For diagnostics, that means writing down reagent behavior, consumable formats, environment, rate at yield, inspection, and data. The URS is not a wish list. If you can’t test a line, it isn’t a requirement.
| URS section | What to write down | What goes wrong without it |
|---|---|---|
| Reagent behavior | Viscosity, foaming, particle suspension, hold time on the line, cleaning between lots | The vendor tests with water and the first real run fails |
| Consumable formats | Every bottle, cartridge, or cap variant and the changeover time per format | Changeover turns into a change order |
| Environment | Humidity, temperature, room class, utilities at your site | The machine passes at the vendor and drifts on your floor |
| Rate | Output at stated yield and uptime, not nameplate speed | You buy a fast machine and run it slow |
| Inspection | What gets checked on every unit and where rejects go | Quality adds a vision station after launch |
| Data | Lot, expiry, UDI, audit trail, and what your MES receives | Labeling gets bolted on at validation |
| Acceptance | A test, a method, and a pass number for each requirement | Everything is arguable at FAT |
Every row needs a matching test and most likely several tests to satisfy. A requirements traceability matrix ties each requirement to the validation test that proves it, per Control Engineering.
Here’s what that looks like in practice. On a scale-up from 70 to 200 PPM, I wrote automated pump calibration, 100% fill volume inspection, 100% print vision inspection, and 100% torque verification into the URS before a single quote came back. The first 200 PPM machine finished with no change orders. The URS was tight enough that I used it to grade the quotes. A few vendors declined to quote at all, because they couldn’t support the documentation.
Score vendors on process proof, not the lowest bid
Score each vendor against the URS using weighted criteria you set before quotes arrive. Weight process experience with your kind of reagent, documentation support, and maintainability above price. Lowest-bid awards tend to come back as change orders.
I’ve watched a lowest-cost award chosen by management, against the analysis, land about a year and a half late and way over budget. The change orders did it. The vendor had overstated its skills.
Build your scorecard from these.
- Evidence they’ve run your reagent type, or a close cousin, on real equipment
- Documentation they can actually deliver, with traceability to your URS
- A habit of testing against the URS before they call you for FAT
- A design a maintenance tech can service without pulling the machine apart
- Quote lines that map to URS lines, so nothing hides in an exclusion
- Named staff who’ll still be on the project in month six
Challenging steps that PAR Systems lists for diagnostic work include accurate dispensing of liquid or dried reagents and bonding or sealing without hurting fluidic integrity. Ask each vendor to show you a run on those steps.
One more rule. Don’t let the vendor write your URS. They’d be specifying a machine they plan to build. That’s a conflict of interest.
On an 80 PPM assembly line, I chose among three quotes with a Kepner-Tregoe analysis. Those machines later ran at 95% uptime, 24/7. Quick consumable change-outs, a maintainable design, and clean documentation got them there.
Make the FAT earn its place in the contract
A factory acceptance test is a witnessed test at the vendor’s site against the URS before the machine ships. It should run an approved protocol with measurable pass criteria. Put the protocol, the criteria, and the punch-list rules in the purchase order.

SG Systems lists a scripted walk-through with no pass/fail evidence as a common FAT failure. I’d add one more. Good vendors have already run the machine against the URS within the FAT document before they call you. A weak one calls you over when 30 to 40 percent of the URS was never addressed. The FAT testimonials tell you whether you want to work with that company.
The full test list lives in the FAT document for diagnostic equipment. The next step, SAT vs. FAT, explains what happens once the machine lands.
Build, buy, or outsource the first volume
Pick the route by how proven your demand is. Automate when the numbers justify it, not when the roadmap feels exciting.
| Route | Best for | Watch for |
|---|---|---|
| Buy custom equipment | Steady volume on a product with a long life ahead | Long lead time, and validation is on you |
| Contract manufacturer first | Launch volume before demand is proven | One pilot-line provider says dedicated lines make sense only once your market position is established and volume exceeds capacity. |
| Semi-automated bridge | Rising volume with formats still changing | Hahn Automation suggests automating the critical steps first and expanding as demand grows. |
Builders such as Labman sell semi-automated vial filling, sealing, capping, and printing systems for immunodiagnostic kits. That’s the middle road in action.
Best for manufacturers moving a diagnostic product from R&D into production, with a process that was never written for automation. Scenario one. You have a foamy or viscous reagent and a stock filler quote. Write the reagent into the URS first. Scenario two. Volume is rising but formats keep changing. Start semi-automated and automate the critical steps. Scenario three. You’re comparing three quotes and can’t tell them apart. Build the scorecard from your URS.
Where to start
Get the URS right and the rest gets cheaper. Write it around the reagent. Grade vendors on what they’ve proven. Hold the FAT to the document.
If you want a second set of eyes, a 30-minute Manufacturing Automation Assessment is the easy way in. We look at your product, your volume, and where the unknowns are hiding. No pitch deck.
Questions buyers ask before the RFQ
What does consumable diagnostics automation include?
Filling, capping or sealing, assembly, labeling, inline inspection, and packing for test kits, cartridges, and lab-use components. Some lines are fill and finish. Others are dry assembly with welding, laser cutting, and leak testing.
Do I need a cleanroom for a test kit line?
Not always. Dry rooms, controlled humidity or controlled environments are common, and one builder runs rapid-test assembly without a clean room but a controlled environment. Open fluidics may need tighter control, so let your risk analysis decide.
Is a fractional automation engineer better than a full-time hire?
Depends how often you buy. A full-time hire fits a company buying equipment every couple of quarters. A fractional engineer fits one buying a line every two or more years, because you add senior experience for the project and the internal team takes over sustaining.
Should my vendor write the URS?
Should not. They’d be writing requirements for a machine they intend to build, and the requirements will drift toward what they already make.
When does semi-automation beat full automation?
When volume is rising but formats or demand are still moving. Automate the critical steps, keep operators on the rest, and expand once the numbers hold.
How long should a FAT run?
There’s no standard. Control Design says each FAT depends on the equipment and the customer’s requirements. My first one took a week just to map the HMI.
The Bottom Line
Get the URS right and the rest gets cheaper: write it around the reagent, grade vendors on what they have proven, and hold the FAT to the document.
Reza Bashar at MEPSCo GAMP provides fractional automation engineering for medical diagnostic manufacturers, from URS development through IQ/OQ/PQ. If you are planning an automation project, reach out directly.