Factory Acceptance Testing and Site Acceptance Testing for Medical Device Manufacturing
Factory Acceptance Testing (FAT) and Site Acceptance Testing (SAT) are the formal verification steps that confirm manufacturing equipment performs to its specified requirements — first at the vendor’s facility, then at the manufacturer’s site. In medical device manufacturing, a properly executed FAT and SAT, documented against the URS and traced through to IQ/OQ/PQ, is the difference between equipment that gets released on schedule and equipment that fails validation after it’s installed.
Most manufacturers think FAT is a formality.
Show up at the vendor’s facility. Watch the machine run. Sign off. Ship it.
That’s not a FAT. That’s a demo. And the difference between a demo and a properly executed Factory Acceptance Test shows up six months later when the equipment is installed, the IQ/OQ/PQ is underway, and requirements that weren’t tested at FAT are now failing in the manufacturer’s facility — on the manufacturer’s timeline, at the manufacturer’s cost.
Problems caught at FAT are fixed at the vendor’s facility, on the vendor’s time. Problems caught at SAT or during IQ/OQ/PQ are fixed on the manufacturer’s time, with production already at risk and the project already behind schedule. Every problem that slips past FAT gets more expensive to fix.
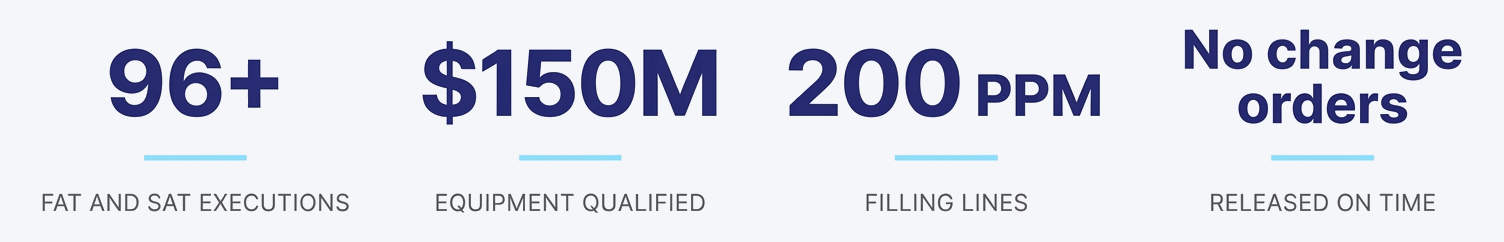
MEPSCo has executed FAT and SAT across 96+ medical device equipment procurement projects. The process comes from the GAMP Documentation Services framework built at Gen-Probe in 2001 — tested on every project since, including $150M in equipment qualified for a DOD pandemic contract with no change orders. FAT and SAT aren’t afterthoughts. They’re the verification layer that the URS was written for.
What Actually Happens at a Weak FAT
Three scenarios. All common. All avoidable.
Scenario 1: No test protocol.
The manufacturer arrives at the vendor’s facility with a list of things they want to see the machine do. The vendor runs a demonstration. Everything looks fine. The machine ships. During IQ/OQ/PQ, the test protocol reveals six requirements from the URS that were never tested at FAT — two of which the machine doesn’t meet. The vendor issues a change order for modifications. The IQ/OQ/PQ timeline slips by 8 weeks.
Scenario 2: Protocol exists but isn’t tied to the URS.
The test protocol covers general machine functions but doesn’t trace back to the specific requirements in the URS. The trace matrix has gaps. During FDA inspection, the quality team can’t demonstrate that the machine was tested against the specified requirements. That’s a 483 observation.
Scenario 3: FAT passed, SAT skipped.
The machine performed correctly in the vendor’s environment. After shipping and installation, the machine doesn’t perform correctly in the manufacturer’s environment — different utilities, different ambient conditions, different operator interaction. No SAT means those issues weren’t caught before IQ/OQ/PQ began. Now IQ/OQ/PQ fails, the vendor has to come back, and the timeline is gone.
None of these are edge cases. They’re standard outcomes when FAT and SAT aren’t executed with documentation tied to the URS.
What a Properly Executed FAT Covers
FAT is not one thing. It’s a collection of verification activities executed before the equipment leaves the vendor’s facility. Each has a specific purpose and a specific documentation requirement.
Test method development. Before FAT begins, every test that will be executed at FAT is documented — what will be tested, how it will be tested, what constitutes a pass, and which requirement in the URS each test verifies. No tests should be improvised at the vendor’s facility.
Functional testing against the URS. Every requirement in the URS is tested and documented. Not a sample. Not a demonstration of representative functions. Every. Requirement. The trace matrix is updated to show which test verified which requirement.
Performance verification. Speed, throughput, fill volume accuracy, capping torque, vision inspection accuracy, HMI function, alarm response, E-stop behavior — whatever the URS requires the machine to demonstrate, it’s tested and documented at FAT.
FAT punch list. Items that don’t pass FAT aren’t reasons to fail FAT — they’re entries on the punch list. Every punch list item is documented with a description of the deficiency, the required resolution, and the responsibility for resolution. FAT closes when every punch list item is resolved, not when most of them are.
Documentation package. The FAT produces a documentation package: the test protocol with results, the punch list with resolutions, and the trace matrix update. This documentation feeds directly into the SAT and IQ/OQ/PQ packages.
What SAT Adds That FAT Can’t
FAT happens at the vendor’s facility. The vendor controls the environment.
SAT happens at the manufacturer’s facility, after the equipment has been shipped, installed, and connected to the manufacturer’s utilities. It verifies that the machine performs correctly in the actual production environment — not in a controlled vendor demonstration environment.
What SAT catches that FAT doesn’t:
- Utility connections that don’t match what the machine expects (compressed air pressure, electrical supply, water quality)
- Environmental conditions that affect performance (temperature, humidity, ambient particulate)
- Operator interface issues that only appear in a real production workflow
- Equipment interactions — how the new machine performs when connected to upstream and downstream equipment in the actual line
SAT uses the same protocol structure as FAT: documented tests tied to the URS, a punch list for items that don’t pass, and a documentation package that updates the trace matrix. It’s the second verification layer before IQ/OQ/PQ begins.
Skipping SAT because the machine passed FAT is how manufacturers end up with IQ/OQ/PQ failures that require the vendor to return to site. The travel cost and timeline impact alone typically exceeds the cost of running a proper SAT.
How MEPSCo Executes FAT and SAT
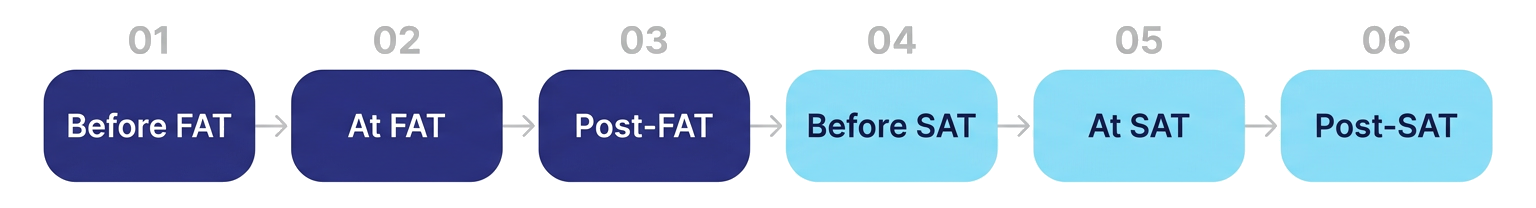
Before FAT
Test method development starts before the travel date. Every test is documented. Every acceptance criterion is defined. Every URS requirement is mapped to a test. The test protocol is reviewed by the manufacturer’s quality team before it’s executed — not assembled at the vendor’s facility on the morning of FAT.
At FAT
MEPSCo runs the protocol. Every test is executed, results are documented, and pass/fail determinations are made against the defined acceptance criteria. Items that don’t pass go on the punch list immediately — not noted mentally and resolved informally. The vendor knows what needs to be fixed and when.
Post-FAT
Every punch list item is tracked to resolution. FAT doesn’t close until every item is resolved and documented. The FAT documentation package is complete before the machine ships.
Before SAT
SAT protocol is developed based on the FAT results and any site-specific conditions identified during installation. The protocol covers the same URS requirements as FAT, with additional tests specific to site conditions.
At SAT
Same protocol discipline as FAT. Every test documented. Every punch list item tracked. SAT closes when every item is resolved.
Post-SAT
The complete FAT and SAT documentation package — test protocols with results, punch lists with resolutions, trace matrix updates — is ready to feed into the IQ/OQ/PQ qualification package. No gaps in the documentation chain.
Proof
On the DOD pandemic project, multiple 200 PPM filling lines were FAT’d and SAT’d in the US and the UK unit was qualified remotely — because the test protocols and documentation were thorough enough to support remote execution without compromising the verification standard. Every machine was validated and released to manufacturing on time. $150M in equipment. No change orders.
“His proficiency in executing Factory Acceptance Tests, Site Acceptance Tests, Engineering Studies, IQ, OQ, and PQ has ensured that our systems meet and exceed regulatory standards, including FDA and GHTF process validation guidance.”
FRANK MAJDI · DIRECTOR OF QUALITY ENGINEERING, HOLOGIC
96+ FAT and SAT executions. The pattern recognition from that volume means the problems that commonly get missed — punch list items that get closed informally without documentation, site condition differences that affect performance, operator interface issues that only appear in production — are caught before IQ/OQ/PQ begins.
When MEPSCo Gets Involved in FAT and SAT
The right engagement model is from the URS forward. When MEPSCo writes the URS, develops the FRS and FDS, and manages the vendor through the build, FAT and SAT execute against documentation that was built for that equipment from the beginning. The trace matrix is already populated. The test protocol development starts from a known set of requirements. Nothing has to be reverse-engineered.
But FAT and SAT support is also available as a standalone engagement.
If a manufacturer has a vendor relationship already in place and needs documentation support and execution oversight for FAT and SAT — without bringing MEPSCo in from the URS stage — that’s a viable engagement. The test protocols are developed from whatever URS documentation exists, gaps are identified and addressed before the FAT date, and the FAT and SAT are executed with the same documentation discipline.
The earlier in the project MEPSCo is engaged, the cleaner the FAT and SAT. But later engagement is better than no engagement.
“Our vendor runs the FAT. We just show up and review.”
Vendors run demos. A FAT executed by the vendor, against the vendor’s test protocol, with the vendor’s pass/fail determinations, is a vendor demonstration with documentation.
The manufacturer needs their own engineer in the room who isn’t the vendor — someone whose job is to verify the machine meets the manufacturer’s requirements, not to sign off on the vendor’s interpretation of those requirements. When the same organization runs the FAT and built the machine, nobody is independently checking whether the requirements are actually met.
That’s not a conspiracy. That’s an incentive structure. The vendor wants to ship. The manufacturer needs to verify. Those aren’t always the same thing.
“We’ve always done it this way and it’s worked.”
Until it doesn’t. One IQ/OQ/PQ failure that requires the vendor to return to site, modify the machine, and re-execute qualification costs more in timeline and budget than running a properly documented FAT and SAT on every project for the next five years. The project that “worked” with an informal FAT often worked because the problems were small enough to absorb. The ones that didn’t work are the ones that produce the war stories.
Common Questions
What is a Factory Acceptance Test in medical device manufacturing?
A Factory Acceptance Test is a formal verification of manufacturing equipment at the vendor’s facility before it ships. Every requirement in the URS is tested against the machine’s actual performance. Tests are documented against defined acceptance criteria. Items that don’t pass go on a punch list that must be resolved before FAT closes. The FAT documentation package feeds directly into the trace matrix and IQ/OQ/PQ qualification.
What is the difference between FAT and SAT?
FAT verifies equipment performance at the vendor’s facility before it ships. SAT verifies equipment performance at the manufacturer’s facility after it’s been installed and connected to the manufacturer’s utilities and production environment. FAT catches build-related deficiencies. SAT catches installation and site-specific issues that only appear in the actual production environment. Both are required for a complete verification chain before IQ/OQ/PQ.
Can FAT and SAT be done remotely?
FAT can be partially supported remotely — video review of certain tests, remote review of documentation — but physical presence for functional testing and punch list assessment is standard for complex equipment. Remote SAT support is more common for replicate machines in facilities where the first unit was already qualified on-site. On the DOD pandemic project, the UK unit was supported remotely because the URS and FAT documentation from the US machines were thorough enough to support remote execution without compromising the verification standard.
What goes on the FAT punch list?
Any test result that doesn’t meet the acceptance criteria defined in the test protocol, any URS requirement that wasn’t demonstrated, any safety or operational issue observed during testing, and any documentation gap that would affect trace matrix completeness. Punch list items aren’t failures — they’re documented deficiencies that the vendor is required to resolve before the machine ships.
How does FAT documentation connect to IQ/OQ/PQ?
The trace matrix links every URS requirement through FAT and SAT test results to the corresponding IQ/OQ/PQ qualification step. When FAT and SAT documentation is complete and tied to the URS, the IQ/OQ/PQ qualification starts from a known baseline — every requirement has been tested, documented, and resolved. When FAT and SAT documentation has gaps, IQ/OQ/PQ has to address those gaps during qualification, which extends the timeline and creates 483 exposure.
What happens if the machine fails FAT?
FAT failure means requirements weren’t met. The vendor fixes the deficiencies, and FAT is re-executed against the punch list items. This is the correct outcome — catching failures at the vendor’s facility, on the vendor’s timeline and cost, is exactly what FAT is designed to do. A FAT with no punch list items on a complex piece of equipment is more suspicious than reassuring. It usually means not enough was tested, not that everything is perfect.
Related Pages
A problem caught at FAT costs the vendor time. A problem caught during IQ/OQ/PQ costs the manufacturer time, budget, and production schedule.
The math on this is straightforward. If your team is approaching FAT or SAT on an automation project and needs documentation support and execution oversight, the assessment call is the right starting point.
Not ready to talk yet? Download the GAMP Roadmap to see where FAT and SAT fit in the full procurement process.